A Clear Look at Reuse Systems
A Clear Look at Reuse Systems
Dynatec has completed over a hundred wastewater purification and reuse systems for industry and for sanitary waste. To begin, there needs to be a detailed characterization of the wastewater along with a detailed characterization of the requirements for reuse. The characterization of the wastewater and requirements for reuse will determine the treatment/purification requirements and thereby define the CAPEX and OPEX. This estimate of costs should be completed early in the process to determine if the reuse project has merit and is cost-effective.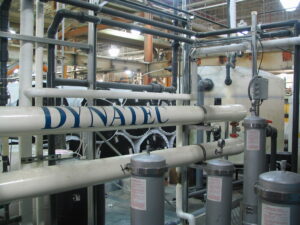
All of Dynatec’s treatment and reuse systems employ membrane filtration because the properly selected membranes provide the best method of insuring the qualitative result desired and in almost every case they provide the most cost effective method of achieving the desired result.
Membrane selection is based upon wastewater characteristics and the desired recovered water quality requirements in the process in which the membranes are utilized.
With the above information, treatability work is typically conducted to define the treatment system requirements and design parameters.
Typical wastewater treatment/purification systems for reuse are as follows.
- Purification of process baths/tanks for reuse typically using ultrafiltration
- Cleaning tanks with contaminants removed employing Ultrafiltration
- Scrubbers with contaminants removed employing Ultrafiltration
- Vibratory metal finishing with contaminants removed employing Ultrafiltration
- Any other employing UF and RO filtration to produce higher quality water for reuse
- Recovery of specific components found in the wastewater
- Precious metal recovery employing Ultrafiltration, Nanofiltration and/or Reverse Osmosis
- Latex paint recovery employing Ultrafiltration
- Textile size separation and recovery
- Others where removal of water allows concentration of the product to be recovered
- MBR biological treatment for reuse in cooling towers, scrubbers and like type water users that do not require potable water or high-purity water
- Food processing facilities where MBR permeate is used in cooling towers and scrubbers
- Metal working facilities where MBR permeate is used in cooling towers and scrubbers
- General manufacturing
- MBR biological treatment followed by Nanofiltration or Reverse Osmosis
- All types of manufacturing and food processing facilities where there is a requirement for higher purity water for reuse.
https://www.dynatecsystems.com/technologies/recovery-and-reuse/
MBR RO for Reuse
MBR RO for reuse, A domestic manufacturer of personal protective equipment is undergoing a major plant expansion. The company now needs to treat their wastewater for reuse as they discharge to a small POTW that could not handle the new volumes or contaminant loading. The new wastewater treatment plant is being built in stages. The first system is a relatively small MBR to handle the first phase of their expanded production. The second system is designed to handle their full-scale production, which will only be several months after the first phase is completed. This system includes an EQ tank, MBR with pre and post anoxic tanks and tubular UF, and RO. The system is designed so that all the RO permeate can be reused while the RO reject can be discharged to the local POTW. One of the goals of the MBR is to reduce nitrates from a high initial concentration to very low levels so that the RO reject will meet that total nitrogen limits for discharge to the POTW. The plant is designed so that future expansion is easily achieved. 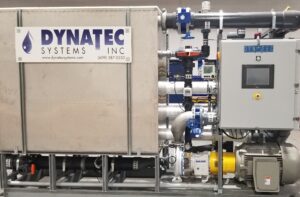
Recovery and reuse systems have been provided by Dynatec Systems to many industries. The ability to recover and reuse water has many benefits.
- Saving on water costs
- Saving on wastewater disposal charges
- Decreased environmental impact
- Protection from regulatory changes
- Decrease dependence on water provider/source
- Ability to expand without affecting water demand
- Overcome water scarcity issues
- Consistently high-quality for water reuse
Ultrafiltration (UF), Membrane Bioreactor (MBR), Nanofiltration (NF) and Reverse Osmosis (RO) are employed by Dynatec for water reuse projects. Water recovery and water reuse has been successfully implemented with industrial and sanitary wastewater streams for: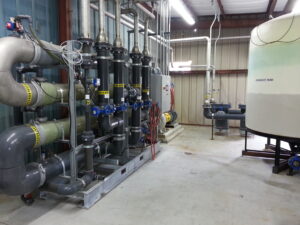
- Cooling tower make up
- Boiler feed
- Irrigation
- Toilet flushing
- Direct potable reuse
- Cleaning/wash applications
- Rinse processes
- Painting processes
- Other plant processes
Recovery and reuse systems provided by Dynatec Systems:
- Resorts, hotels, and retirement homes
- Golf courses
- Automotive companies
- Food and beverage companies
- Apartment buildings
- Landfills
- Mines
- Metal finishing plants
- Aerospace companies
For more information about wastewater reuse, contact us today.
https://www.dynatecsystems.com/technologies/recovery-and-reuse/
Contract Service – DBOOM
A contract service – (DBOOM) system owned and operated by Dynatec has now been in operation for 30 years. The system was provided to the customer, a manufacturer of bearings, on a Design, Build, Own, Operate, Maintain (DBOOM) basis. Dynatec designed and installed the system 30 years ago and has been operating and maintaining it since. The customer pays Dynatec a few cents per gallon of wastewater treated. The DBOOM arrangement has been an attractive option to several customers over the years. It allows them to achieve the wastewater treatment goals without a capital expenditure and without operating and maintenance responsibility. Another Dynatec system has been successfully operating on a DBOOM basis at a large automotive company’s stamping plant for 22 years.
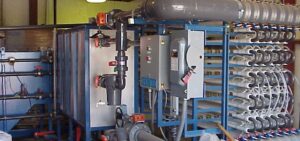
Design-Build-Own-Operate-Maintain complete wastewater treatment system solutions offers the assurance of a well-run operation with little risk and no capital required.
Complete Wastewater Solutions
Since 1978, Dynatec has supplied complete wastewater treatment systems for industrial applications and in that time, we have successfully installed over a thousand systems. Since 1993, we have provided DBOOM solutions that are completely designed, built, owned, operated and maintained by Dynatec.
Contract Service (DBOOM) benefits: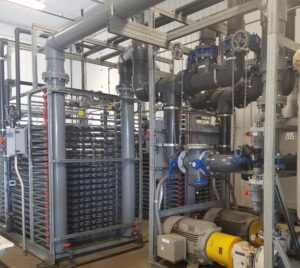
Little Risk
Get the assurance you need for a well-run and well-operated system. Offering minimal risk with great convenience to the customer. Dynatec owns, operates and maintains the equipment, supplying complete wastewater treatment systems on a contract basis. Each contract is tailored to the owner’s unique requirements.
Cost-effective
Our contract service agreements offer a reliable means of both reducing and fixing costs. This allows our clients to accurately predict operating costs and provide the option for purchase of the system at the end of the contract term.
Compensation, in the form of monthly payments, is based on the amount of water treated, purified and discharged to sewer or reused. The per-gallon charge fixes the total cost for processing the waste stream.
Minimal Liability
With minimal operator attention required, a locally-employed Dynatec technician will attend to the system on a daily basis to check for proper functioning, the need for service or maintenance and water quality.
Your Dynatec technician covers all attention, care and maintenance required by the system to ensure compliance with sewer discharge standards. Contaminants removed are disposed of through an approved and licensed disposal firm.
Contract Service – DBOOM project begins the same way all of our projects start. First, we obtain thorough information that helps us characterize your waste stream and the treatment requirements. Once treatability work is performed, we develop a system design and proposal. At that time, the terms of the contract can be negotiated. Dynatec can confirm the project requirements, and implement on-site pilot testing, when necessary.
Contract Service – (DBOOM)
- No risk
- No capital employed in non-performing assets
- No need to operate or maintain equipment
- Assurance of a well-run and well-operated system
- Significant cost savings
- If waste is presently being hauled to a commercial waste treatment facility, this program will help to considerably reduce costs.
- Costs fixed for the term of the contract
- Lower environmental liability
For more information about Dynatec Systems’ (DBOOM) Design-Build-Own-Operate-Maintain services, please contact us to discuss your opportunity.
Decentralized Wastewater Treatment Facility
Dynatec provided the membrane system for a demonstration plant situated directly adjacent to the Anaheim, CA City Hall. The system is designed to pump wastewater from a local sewer line, treat the wastewater for reuse, and return the waste activated sludge and screenings to the sewer line.
The DynaLift™ out-of-basin membrane system was selected because:
- The high flux rates achieved by the DynaLift™ system allowed for a small footprint
 High MLSS concentrations allows for smaller reactor tanks
- The positive filtration achieved with MBR provides consistent high-quality discharge
- The out-of-basin design allows for better demonstration of the technology
- The membrane construction allows for high removal of bacteria and virus – demonstrated 5-log removal of bacteria and 4-log removal of virus.
The plant design is for two trains with the first train presently installed. The design flow of this plant is 75,000 gallons per day, and due to internal water uses, such as screen flushing, the net output of the final plant when fully installed will be 104,350 gallons per day. The recycled water is used for irrigation and toilet flushing within the requirements of California’s Title 22 Regulations.
Plant automation design allows for periodic operator attention only when equipment maintenance or chemical refilling is required.
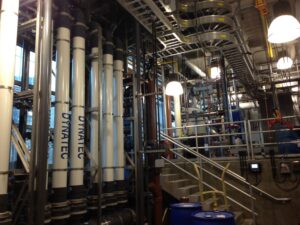 Following treatment in the MBR, the effluent is further treated using ozone followed by UV for ozone destruction and chlorine addition at 1 mg/L to ensure no re-growth in the final effluent.
Due to the proximity of City Hall and the fact that the plant is in a highly populated area, a state-of-the-art odor control system was installed. With the standard Dynatec design odor control is not typically required.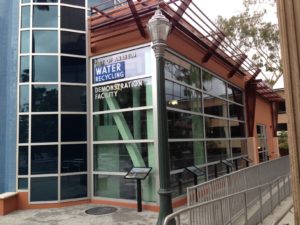
This is the first facility in California to use external MBR membranes, ozone and chlorination for water recycling. The use of decentralized wastewater treatment facilities is increasing and the City of Anaheim is in the forefront of this.
Contact Dynatec Systems today to discuss your wastewater reuse project.
https://www.dynatecsystems.com/industries/sanitary-wastewater/
MBR Conversion – Pharmaceutical Company
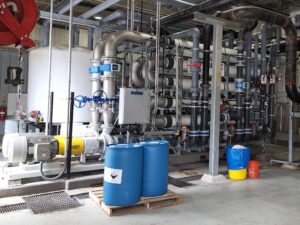 A pharmaceutical firm suffered from frequent upsets to their existing treatment process. The existing conventional aerobic biological system followed by a gravity clarifier, led to discharge noncompliance.
Dynatec completed bench top treatability studies and pilot studies to confirm the best method to improve performance. Adding ultrafilters as part of the conversion to a Membrane Bioreactor (MBR) was the best course of action.
MBR Conversion – Pharmaceutical Company
The wastewater stream was high in organic content (BOD, COD), and suspended solids (TSS). The MBR conversion, using a Dynatec ultrafiltration system allowed the customer to run the biological system at high mixed liquor concentrations without concern for settling characteristics. The higher mixed liquor concentration and longer sludge age proved to be successful in consistently reducing BOD and COD into compliance.
The system was designed to treat nearly 300,000 gallons per day. The COD was consistently reduced to 300 – 500 mg/l from 14,000 mg/l while BOD was reduced to non-detect.
The upgraded system handled variable loads in terms of organic load and flow rates. It consistently delivered high-quality effluent with less operator attention than their previous system. Additionally, the customer no longer faced fines for exceeding discharge limits for organics and solids.
Dynatec completed the process design, provided the equipment, and performed the installation. Existing tanks and aeration were utilized, keeping the conversion cost to less than any alternative.
Dynatec Systems industry-leading tubular ultrafiltration (UF) system can be used to treat a broad range of industrial wastewater by separating insoluble components from waste streams. As a cost effective and simple solution for separating insoluble components and colloidal contaminants from a waste stream. Wastewater ultrafiltration offers significant advantages over conventional separation. It is a useful process that does not require chemicals or much space to separate insoluble contaminants.
Contact Dynatec to discuss your wastewater treatment needs.
https://www.dynatecsystems.com/technologies/membrane-bioreactors/mbr-conversion-r…pgrade-solutions/
Data Center Water Management
As data centers continue to expand in water-stressed regions and face limited capacity at public treatment works (POTWs), the need for onsite water reuse has never been greater. Dynatec’s membrane treatment systems provide a reliable, high-efficiency path to sustainable water reuse. Our systems reduce consumption, mitigate risk, and support sustainability initiatives.
Challenges Addressed
• Water Scarcity – Increasing water use restrictions in arid regions
• Limited POTW Capacity – In some areas, municipal treatment plants don’t have the ability to accept the high volumes of wastewater produced at data centers
• Corporate Sustainability Mandates – Rising pressure to meet water reduction targets, achieve LEED or Green Grid benchmarks, and align with global ESG goals
• Water Mining Opportunities – Capture and treat alternative water sources to offset potable use
Dynatec Membrane Technologies for Water Reuse
Our systems treat and reclaim wastewater. The high-quality water produced is suitable for reuse, including cooling applications.
System Technologies
• Ultrafiltration (UF) Removes suspended solids, organics, and microorganisms to protect downstream systems.
• Reverse Osmosis (RO) Reduces total dissolved solids (TDS) and chlorides. Produces high-purity water ideal for cooling tower reuse.
• Ultra-High Pressure RO (UHPRO) Concentrates RO reject up to 1,800 psi, enabling high recovery and reduced brine volumes—ideal for ZLD or minimal liquid discharge (MLD) strategies.
• Membrane Bioreactor (MBR) Combines biological treatment and ultrafiltration for compact, robust treatment. Can be used for on-site sanitary wastewater and for water mining in regions facing water scarcity.
Key Benefits for Data Centers
• Significantly Reduce Freshwater Intake Meet or exceed corporate water intensity targets (gallons/MWh).
• Minimize or Eliminate Discharge to POTWs Achieve ZLD or MLD goals. Reduce dependency on local infrastructure.
• Support Sustainability Initiatives Contribute to efforts to achieve LEED, Green Grid, and ESG Metrics.
• Compact, Modular Systems Saves on space and cost. Ideal for retrofits.
• High Reliability for Critical Operations Automated controls, robust materials, maximum uptime and proven designs.
Partner with Dynatec
With over 40 years of experience in industrial membrane systems, Dynatec delivers field-proven water reuse solutions. Our membrane systems are engineered for performance, reliability, and sustainability. Contact us for solutions that meet the demands of modern digital infrastructure
Paint Manufacturer Reuses Latex
A paint manufacturer engaged Dynatec to provide a system to separate latex from wastewater and reuse it in the production of paint
The Problem
The company was using a chemically assisted, rotary drum vacuum pre-coat filter that was expensive to operate and created a lot of sludge which was expensive to dispose.
The Solution
The white paint wastewater was segregated from the colors, and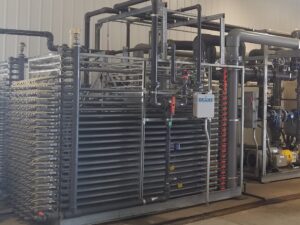 processed separately. The concentrate of white latex solids were used in the manufacture of new white paint.
The paint solids from the colored paints can be concentrated to as high as 20% (typical paint contains between 45% and 55% solids) using wide channel ultrafiltration. The paint solids are concentrated and reused to make a grey paint. The water can be discharged to sewer, since it contains no solids, or it can be reused as wash water.
Special circulation pumps are also used to handle the high solids loadings.
Return on investment
The return on investment was high. The latex from the white paint wastewater is reused in the production process for manufacture of new paint. The paint solids from the colored paint wastewater is recovered as a saleable low quality paint product. The cost for disposal of the solids removed by the old chemical treatment system has been reduced by 90%. The wastewater from both processes is discharged to sewer.
Significant Savings:
No sludge
Beneficial use for latex
Water quality for discharge is better
Much less operator time
No chemicals
Ultrafiltration excels at the clarification of solutions containing:
Suspended solids
Bacteria
High concentrations of macromolecules including:
Oil and water
Fruit juice
Milk
Latex
Whey
Electro-coat paints
Pharmaceuticals
Poly-vinyl alcohol
Potable water
Tertiary wastewater
Some proteins
Some dyes
Oils
Colloidal or emulsified components
Contact Dynatec Systems today to discuss your wastewater solution!
https://www.dynatecsystems.com/technologies/membrane-technologies/ultrafiltration-systems/
Anaerobic MBR with Dynatec Tubular UF Membranes
Maximizing Efficiency & Sustainability in Industrial Wastewater Treatment
Why Choose Anaerobic MBR?
Anaerobic Membrane Bioreactor (AnMBR) technology is revolutionizing industrial wastewater treatment by combining anaerobic digestion with advanced membrane filtration. This cutting-edge process enables industries to achieve superior wastewater treatment while generating biogas for energy recovery.
The Dynatec Advantage: Tubular UF Membranes Dynatec’s tubular ultrafiltration (UF) membranes are at the core of our AnMBR systems, offering unmatched performance in treating high-strength wastewater.
These membranes provide:
Superior Solids Handling –
Handles high mixed liquor suspended solids (MLSS) without frequent cleaning or fouling.
Consistent Permeate Quality –
Achieves exceptional effluent quality with low turbidity and high removal of contaminants.
Robust & Durable Design – Built to withstand challenging industrial wastewater conditions.
Minimized Maintenance – Long membrane lifespan with reduced downtime and lower operating costs.
Key Benefits of Anaerobic MBR with Dynatec UF Membranes
- Energy Generation & Cost Savings
– Converts organic matter into biogas, reducing energy costs.
– Eliminates the need for aeration, lowering power consumption significantly.
- High-Quality Effluent for Reuse or Discharge
– Produces low-BOD and TSS effluent, meeting stringent discharge limits.
– Enables water reuse for non-potable applications, reducing water demand.
- Compact Footprint & Modular Scalability
– Requires less space than conventional anaerobic treatment.
– Easily scalable to meet varying flow rates and loads.
- Low Sludge Production & Reduced Handling Costs
– Generates minimal biosolids, lowering disposal costs.
– Reduces environmental impact and regulatory burdens.
Ideal Applications
– Food & Beverage Processing
– Agriculture / Manure
– Pulp & Paper Mills
– Pharmaceutical & Chemical Industries
– Landfill Leachate Treatment
-High-Strength Industrial Wastewater
Optimize Your Wastewater Treatment Today. Leverage the power of Anaerobic MBR with Dynatec’s tubular UF membranes for a sustainable, cost-effective, and energy-efficient solution.
Contact us today to learn how our advanced wastewater treatment systems can work for you.
Landfill leachate treatment system
Landfill leachate treatment system for a hazardous waste landfill incorporates heavy metals pretreatment followed by a tubular MBR system.
The MBR reduces:
- ammonia
- phenol
- Polychlorinated Biphenyl (PCB)
- chemical oxygen demand (COD)
- volatiles and semi-volatiles
- and other contaminants adequately for discharge
The system reduces PFAS 30-60% and carbon is utilized to reduce PFAS to low ppt concentrations.
Landfill leachate treatment systems with Membrane Bioreactors (MBR)s have developed many unique process improvements for industrial wastewater applications. Dynatec successfully uses Ultrafiltration (UF), MBR and Reverse Osmosis (RO) for landfill leachate applications.
Landfill leachate treatment requirements
Treatment can vary, depending on the discharge requirements, and the contaminants present
Landfill leachate is characterized by: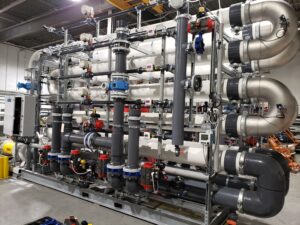
- High Total Dissolved Solids (TDS)
- Heavy metals
- High BOD
- Color
- High COD
- High ammonia
Landfill leachate treatment systems options
The MBR option: an aerated biological mixed liquor process operating at very high solids concentrations.
The advantages are:
- Long sludge age produces a well acclimated biomass. High concentration (typically 12,000 to 20,000 mg/l) provides very high rates of reaction
- Excellent nitrification and de-nitrification
- Smaller footprint then conventional aerated systems
- High-quality effluent as a result of using membranes for final clarification
- Lower sludge production than conventional systems
Typical MBR results in landfills:
| Parameter | BOD | COD | TSS | Ammonia |
|---|---|---|---|---|
| Influent | 500 | 4000 | 150 | 1000 |
| Effluent | <5 | 800 | <5 | <1 |
| % Removal | >99% | 80% | >96% | >99% |
The system produces bio-sludge, which can either be dewatered for disposal, or disposed of as a liquid sludge.
Alternative landfill leachate treatment options:
- Chemical precipitation of metals before MBR treatment
- RO after MBR treatment removes organic and inorganic contaminants, and color
- UF followed by RO
The two effluent streams from a RO system are:
- Permeate
- Concentrate (or reject)
This can be re-injected into the landfill. Its long-term effects on leachate concentrations should be considered.
Conclusion
The MBR process provides the highest possible levels of organic removal with essentially zero suspended solids in the effluent. This is the ideal feed system for RO treatment.
RO permeate can be used for other non-potable purposes:
- Irrigation
- Truck washing
- Dust control
Dynatec membrane treatment systems have successfully provided outstanding performance in many landfill leachate applications. Considerations for this technology include:
- Membrane treatment offers reliable, consistent landfill leachate
- Systems are highly cost effective, and require low levels of operator interface
- The best membrane system configuration for each application should be individually evaluated
- Membrane treatment is broadly applied in the US and abroad
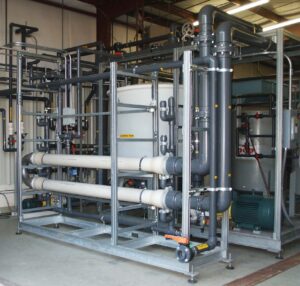
https://www.dynatecsystems.com/industries/landfill-leachate-treatment/
For more information on landfill leachate treatment systems, please contact us today.
Upgrades using existing assets
Upgrades using existing assets
When discharge regulations tighten, the need for water reuse grows, or wastewater volumes increase, existing Sequencing Batch Reactor (SBR) systems often become inadequate. In order to provide a solution with low capital cost in part by reusing existing assets, existing SBR plants can be converted to Membrane Bioreactors (MBR). This can usually be done by adding an out-of-basin tubular ultrafilter (UF) to the process. Using a Dynatec out-of-basin UF as part of an SBR to MBR conversion is the most cost-effective and easy to implement way to:
- Improve biological system performance
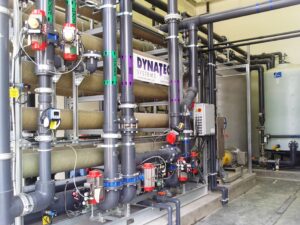
- Expand capacity
- Handle increase in strength of waste
- Mitigate upsets
- Reduce operator time
- Achieve consistent performance
Dynatec has used existing assets from SBR systems to convert to an MBR at many site including at landfills, food and beverage plants, chemical manufacturing, and automotive manufacturing facilities.
The industrial MBR is the ideal bioreactor configuration for treatment of organic or inorganic contaminants present in industrial wastewaters. MBR’s operate at a higher efficiency while achieving consistent design performance objectives. This makes MBR a more cost effective method of industrial wastewater treatment when performance and tank requirements are considered.
Industrial Membrane Bioreactors Benefits:
- Higher flux
- Lower costs
- Better membranes
- Improved permeate quality
- Less operator attention and maintenance
Applications
Dynatec’s industrial MBR is the ideal biological system for industrial wastewater treatment. It is designed to handle high strength wastewater containing high concentrations of:
- Biochemical Oxygen Demand (BOD)
- Chemical Oxygen Demand (COD)
- Oil & Grease (FOG)
- Volatiles
- Metals
- Ammonia
- Nitrate
- Inorganic
The performance is not affected by changes in sludge settleability like the conventional systems, making it the wise choice for industrial wastewater treatment systems that have difficult-to-treat waste streams. Dynatec’s MBRs can effectively handle industrial wastewater streams that would otherwise be toxic or inhibitory to other biological treatment systems.
Backed by decades of experience with MBRs, Dynatec has developed many unique process solutions necessary for industrial wastewater treatment applications such as:
- Landfill leachate
- Hazardous landfill leachate with metals removal
- Automotive manufacturing wastewater
- Food manufacturing wastewater
- Titanium processing wastewater
Contact Dynatec Systems today to discuss your wastewater solution.